Start With the Disc Face, Edge and Date Code
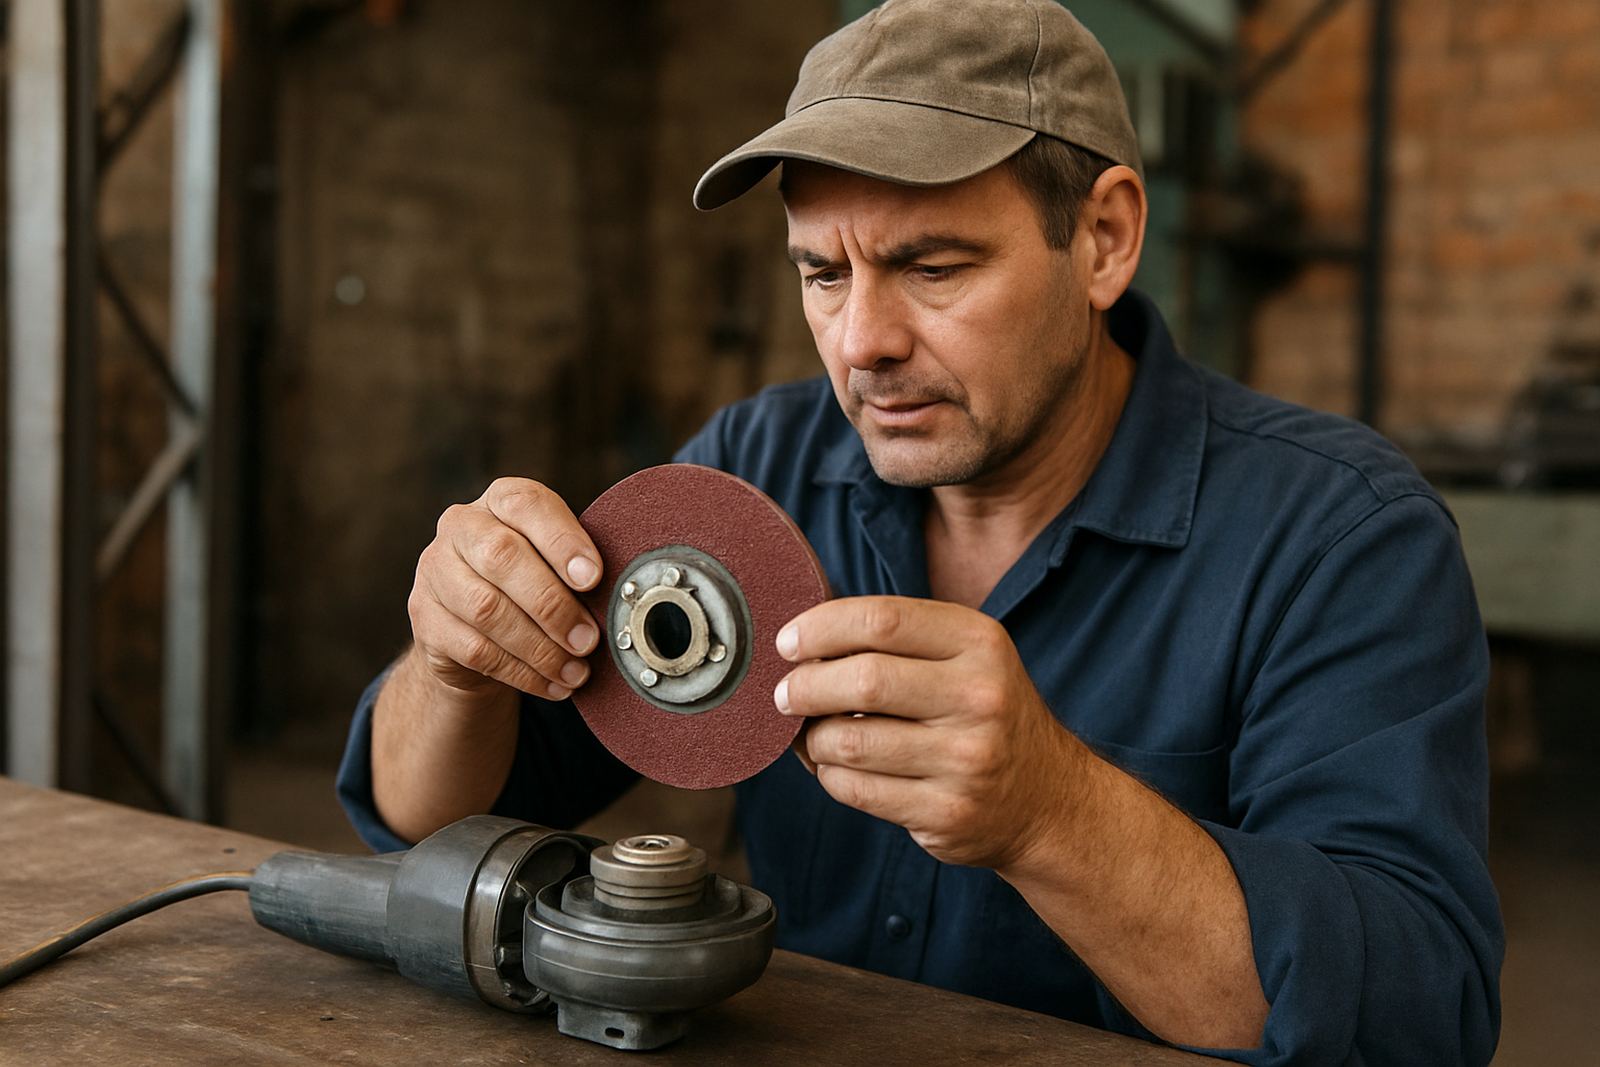
Before fitting a disc, look at both sides for cracks, chips, moisture damage or a glazed patch that shows the disc has been knocked around. If the edge looks uneven or has a white powdery line, set it aside. A disc that has been dropped can fail early, even if the damage is not obvious at first glance.
Check the expiry date or date code where it is printed. Bonded discs do not last forever, especially in a Durban or Pinetown workshop where heat and coastal humidity can work their way into stored stock. Old discs can become brittle and throw off cutting control when the operator puts pressure on the cut.
- Reject any disc with a visible crack or chip.
- Do not use discs that have been wet or stored on damp concrete.
- Keep discs in a dry cabinet or sealed container if possible.
Match the Disc to the Machine and the Material
One of the most common mistakes in trade workshops is using the wrong disc for the machine size or the material thickness. A thin cutting disc meant for mild steel is not the right choice for heavy section work, and a disc rated for a 115 mm grinder will not suit a 230 mm machine. Check the diameter, bore size and speed rating before you start.
The material matters too. Stainless steel, masonry, aluminium and general steel all need different cutting behaviour. Using the wrong disc can overheat the workpiece, slow the cut and leave the disc wearing unevenly. If a disc is not suited to the job, do not force it, because the extra pressure is where trouble starts.
- Confirm the disc speed rating is above the grinder speed.
- Check the bore size is a clean fit on the spindle.
- Use the correct disc type for steel, stainless or masonry.
In a busy New Germany fabrication shop, the operator may be moving between angle iron, box section and sheet metal in the same morning. Keeping the discs grouped by material type makes these checks quicker and helps avoid mix ups, especially when the team is under time pressure.
Inspect the Flanges, Guard and Lock Nut Before Fitting
The disc itself is only part of the setup. A bent flange, damaged guard or loose lock nut can cause vibration that turns a simple cut into a problem. Before fitting the disc, wipe the spindle and flanges clean and look for burrs, rust or swarf that can stop the disc seating properly.
Make sure the guard is in place and set to direct sparks away from the operator and any stored solvent, gas cylinders or cardboard stock. In a small workshop, a poor guard position can send sparks onto the floor or across a nearby bench. It takes seconds to check and can save a lot of grief later.
- Clean the spindle threads before tightening the nut.
- Replace worn flanges that no longer sit flat.
- Set the guard to cover the disc as much as the job allows.
Do a Short Spin Test Before the First Cut
After fitting the disc, let the machine run free for a few seconds before cutting. Stand out of the line of the disc and listen for rattling, a wobble or a change in tone. If the grinder vibrates hard or the disc looks like it is tracking off centre, stop immediately and refit it.
This quick test is especially useful when a workshop has several users sharing machines over a shift. One person may have fitted a disc too tightly, or the spindle may have picked up a bit of debris. A short spin test catches those faults before the disc bites into the work. It is a simple habit, but it saves material and fingers too.
For a site team in Umhlanga doing light maintenance, that extra minute matters because the crew may only have one grinder running while power is off during load-shedding. A free spin check helps avoid wasting the only good disc left in the toolbox.
Watch How the Cut Starts and How the Disc Feels in Hand
The first few seconds of the cut tell you a lot. A healthy disc starts cleanly, without grabbing or burning the edge of the material. If the disc pulls to one side, leaves a rough kerf or throws a shower of sparks in one direction, stop and inspect the setup. The wrong feed pressure or a tired disc can both cause that behaviour.
Keep a steady grip but do not lean on the machine. Let the disc work at its own pace. Pushing too hard overheats the bond and shortens disc life, while also increasing the chance of shatter. A smooth cut should feel controlled, not forced.
- Check for heat build up in the workpiece after the first pass.
- Listen for chatter, squeal or a change in motor note.
- Replace the disc if the cut becomes slow or uneven.
If the operator notices the disc slowing down on mild steel strip, the safest move is to stop and fit a fresh one. Trying to get one more cut from a worn disc often ends up costing more in damaged stock than the disc was worth.
Store Discs Correctly So They Stay Fit for Use
Good cutting disc checks begin long before the machine is switched on. Storage matters. Keep discs flat, dry and out of direct sun. Do not leave them on a workshop floor where moisture from a washing bay or open roller door can creep in. In coastal areas, humidity can spoil stock faster than many teams expect.
It helps to label opened packs by disc type and size so the right one is easy to reach during a busy job. A tidy stock list also makes replenishment simpler when the branch manager or buyer needs to reorder. In workshops around Pinetown, Westmead and Durban North, that small bit of control can cut down on emergency runs to replace damaged discs.
- Store discs flat in their original pack or a dry bin.
- Keep them away from oils, water and welding slag.
- Rotate stock so older discs are used first.
Jameson Tools works with trade workshops, DIY users and setup teams who need practical stock control, not guesswork. If the discs are organised and checked properly, there is less waste and fewer interruptions during the day.